Rapid Prototyping und Direct Manufacturing: 2 Facetten der Generativen Technologien aus Industriesicht
←
→
Transkription von Seiteninhalten
Wenn Ihr Browser die Seite nicht korrekt rendert, bitte, lesen Sie den Inhalt der Seite unten
Rapid Prototyping und Direct Manufacturing:
2 Facetten der Generativen Technologien aus Industriesicht

                                                                      Klaus Müller-Lohmeier
                                                                      Festo AG&Co. KG
                                                                      Esslingen, Deutschland

Symposium „Virtuelle Produktentwicklung“, Rapperswil (CH), 19. April 2012
SI-T/Müller-Lohmeier                                                                           1
Vorbemerkung

SI-T/Müller-Lohmeier   2
Think global, act local

                „ Automation and Didactic                     „ Turnover (Group): EUR 2,1 billion (2011)
                „ Factory and Process Automation              „ 15,500 employees in 176 countries
                „ 300,000 customers                           „ 2,900 patents world-wide
                „ 30,000 catalogue products                   „ R&D budget 8,5 % of sales

                                                   People: our no. 1 success factor

SI-T/Müller-Lohmeier                                                                                       3
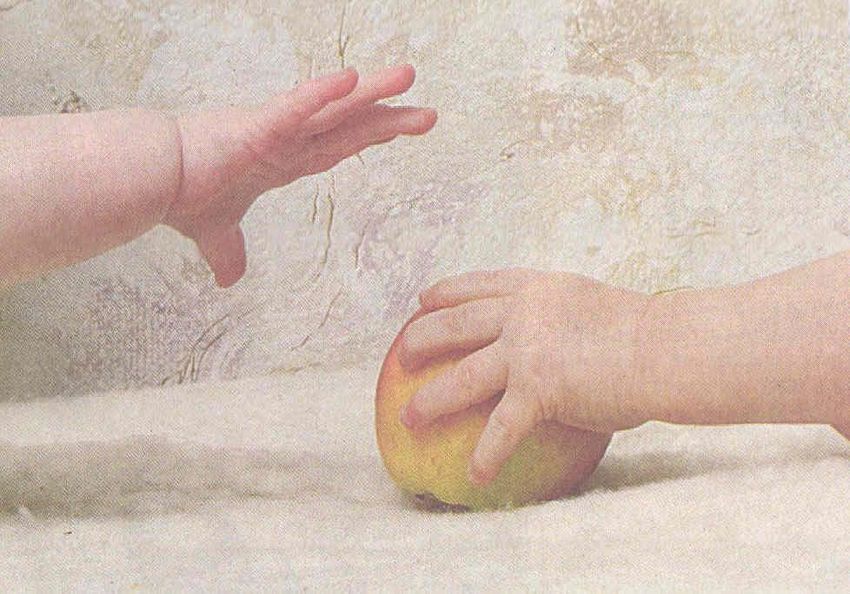
Begreifen – durch begreifen !

                                                 Oft muss man Dinge einfach
                                                 mal anfassen, fühlen, anschauen,
                                                 sich veranschaulichen …

                                                 bevor man weitere Schritte unternimmt
    (Bild-Quelle: Sonntag Aktuell, 31.01.2010)

SI-T/Müller-Lohmeier                                                                     4
Hier kommt das „Additive Manufacturing“ ins Spiel !
 Behauptung: Sie alle hier haben eigene praktische Erfahrungen mit dieser Technologie ! ?

 Top, die Wette gilt !

 Wer von Ihnen hat noch nicht mit Lego gebaut ?

SI-T/Müller-Lohmeier                                                                        5
What is Additive Manufacturing ?
 How generative or layerwise technologies work

                                                 3D-CAD      Postprocessing               Layerwise material
                                                 model as    with                         deposition following
                                                 necessary   (virtual) slicing            the specific slice
                                                 origin                                   information

                                                                                                                 LS(1‘)

    (Bild- + Video-Quellen: Lego; EOS                            The technological path
    Matthes: Grundlagen der Fertigungstechnik)

SI-T/Müller-Lohmeier                                                                                                      6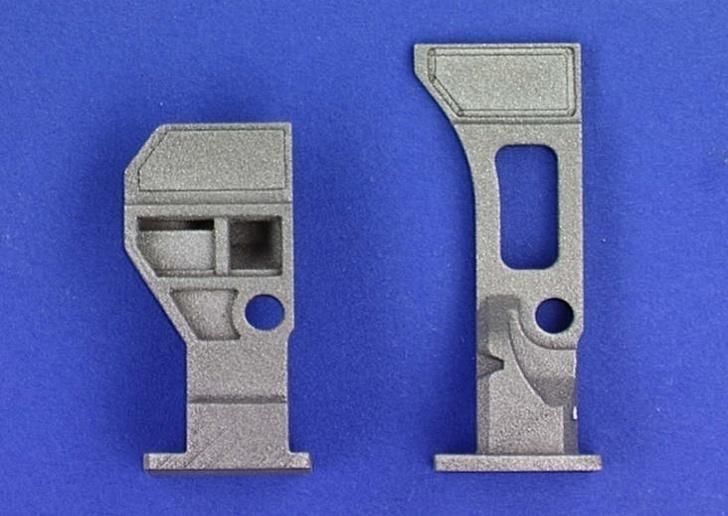
The right way: Additive Manufacturing

   „ Definition according ASTM F2792-10 (F42), 2009:

           "process of joining materials to make objects from 3D model data,
            usually layer upon layer, as opposed to subtractive manufacturing methodologies”

   • Synonyms:

           rapid prototyping, rapid manufacturing,
           additive fabrication, additive processes, additive techniques,
           additive layer manufacturing, layer manufacturing, freeform fabrication

   • similiar definition: VDI 3404:2009-12

SI-T/Müller-Lohmeier
Nomenclature of generative techniques

   „ Rapid Prototyping (RP):
     toolless fabrication of (single) prototype parts in layers
     direct from CAD data
       VDI: Rapid Prototyping (RP)
       Generative Herstellung von Bauteilen mit eingeschränkter Funktionalität (Prototypen, Versuchsteile).
       Eigenschaften: ausgewählte Merkmale, z.B. Geometrie, Haptik. Material kann, muss aber nicht Serienmaterial
       sein. Konstruktion kann, muss aber nicht fertigungsgerecht im Sinne der Serienfertigung sein.
   „ Rapid Manufacturing (RM) / Direct Manufacturing (DM) :
     toolless manufacturing of (small-lot) series of end-use parts
     in layers direct from CAD data
       VDI: Rapid Manufacturing (RM)
       Generative Herstellung von Endprodukten (häufig auch als Serienteile bezeichnet).
       Eigenschaften: Weist alle Merkmale des Endprodukts auf oder wird vom Kunden
       für den „Serieneinsatz“ akzeptiert. Material ist identisch mit dem des Endprodukts.

   „ Rapid Tooling (RT) / Direct Tooling:
     layer-wise, non-cutting (non-eroding) fabrication of
     injection molding or diecasting tools
SI-T/Müller-Lohmeier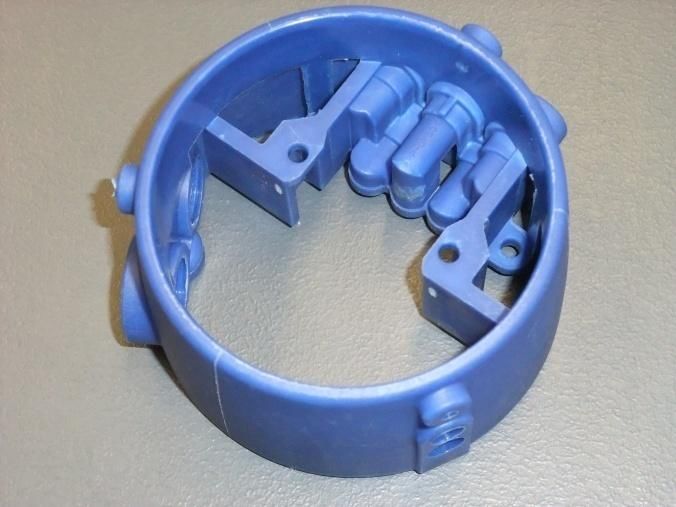
Additive Manufacturing is part of the digital solution process !
                                                 shipment

                          (first) design / CAD              assembly
                                                                                 final AM parts
                                                            reverse
                                                            engineering

                                                                                                          finishing of AM parts
  FEM simulation / virtual reality

                                                                virtual part placement in         layerwise part build-up
                           CAD model -> slice model             build envelope of AM machine      in AM machine
SI-T/Müller-Lohmeier                                                                                                              9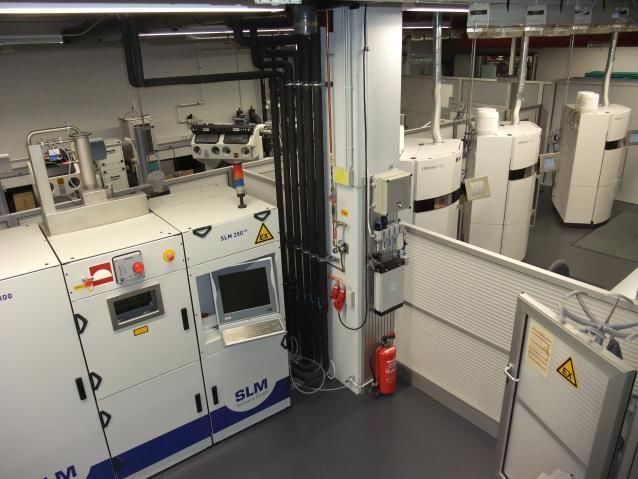
Historisches

    Vom „Spielzeug computerverliebter Ingenieure“…

    1987               In USA auf der "Autofact"-Messe erstmals Vorstellung einer
                       Stereolithografie-Maschine durch die Fa. 3D-Systems
                       (Hull, Patent US4575330, 1986)

    … zum „Standard“-Werkzeug moderner Produktentwicklung

    Mitte 2011         Kumuliert wurden weltweit ca. 40.000 generative RP-Anlagen installiert
                       (Quellen: Wohlers Report, 3D-Schilling, Objet)

SI-T/Müller-Lohmeier
Generative (or additive) techniques at Festo: history and status „ practical own experience in RP techniques since 1995 (8 years after birth of the new technology) „ using nearly all generative techniques available „ network of in-house facilities (4x FDM, 3x SLS, 1x SLA, 2x SLM) -> Festo Fast Factory „ in 2011 some 18.000 parts are realized within more than 1.100 orders „ contact to well-known research instituts „ involved in a couple of research projects „ active member in several AM associations SI-T/Müller-Lohmeier
Festo Fast Factory
Definition
Die Festo Fast Factory (FFF) bildet die technologische Basis für die
Umsetzung von virtuellen Lösungen in physisch-reale Körper.
Sowohl für Kunden als auch für Festo ergeben sich mit dieser effizienten
Prototypen-Herstellung in der individuellen Produktentwicklung enorme
Einsparungspotenziale, die das Time-to-market deutlich reduziert.
In beiden Fällen geht es um die schnelle und werkzeuglose physische Realisierung von Ideen/
Lösungsansätzen/-alternativen als Basis für weitere Schritte / Entscheidungsprozesse
Erst-Verfügbarkeit von neu entwickelten Einzelteilen, Baugruppen oder Lösungskonzepten
in Stunden und Tagen anstatt Monaten oder Quartalen
SI-T/Müller-LohmeierMission 1: Support Festo customers
Market requirements
Realisation of customer specific solutions
within shortest possible time
Partnership
Engineering together with customers by
continous interaction (from 3D-models over
simulation to rapid prototypes)
Speed is a competitive advantage !
Fast realisation of adequate customer solutions
SI-T/Müller-Lohmeier 13Mission 2: Accelerate Festo R&D
Decrease time to market for catalog products
Especially tool based parts show often long
delivery times
Usage of alternative manufacturing
technologies allows to cut lead times for
specific parts
Fast availabilty of functional prototypes
yields to earlier realiabilty in the design
process
R&D advantage through speed improvement
in technical conversion of a solution !
Fast supply of design and functional prototypes for R&D
SI-T/Müller-Lohmeier 14Case study: Short run production of customer specific parts
Customized holding fixtures for gripper elements (FDM, ABS)
Continous request from sales department / market
On-demand toolless production of customer specific polymer grippers
Average time for completion of small series < 1 day; average delivery time < 3 days
Customer orientation
SI-T/Müller-Lohmeier 15Case study: Customer problem solution
Customer specific cylinder (SLS, PA 12)
Short-time delivery (< 3 days) of alternative cylinder body geometries
External: quick delivery to customer for implementation studies
Internal: fast available prototypes for internal pressure creep test yielding for safety in providing
alternative solutions (more than 3 months at 10 bar and 80°C)
Quick customer support
SI-T/Müller-Lohmeier 16Case study: Customer specific development
Pilot valve for valve control unit
concept model for customer development discussion
toolless production of a series of 5 units within 2 days
avoiding tool costs in case of wrong development direction
Fast supply of customer specific concept models
SI-T/Müller-Lohmeier 17Case study: Direct / Rapid Manufacturing
Fastener for flexible tube (Tripod project) Coil body for Didactic project
typical annual demand: 300 / 800 pieces
toolless production by plastic laser sintering (SLS) within < 2 weeks
costs less than € 3 / piece
Economic short run production of accessories and basic parts for new concepts
SI-T/Müller-Lohmeier 18Case study: Serial production of polymer parts
Snap-fit for serial supply of a major customer (SLS, PA 12)
Additive fabrication of 12.000 snap-fit (alternative technology !)
Complete process chain (with 4 build chamber fillings) realized within 37 hours
Plastic injection molding vs. toolless additive fabrication:
time 2 months vs. 2 weeks, costs 1 : 0,66
Top speed for customer satisfaction
SI-T/Müller-Lohmeier 19Case study: Laser melted steel parts
Drive part prototyping for R&D
Left Right
stop stop
Stop parts for a new generation of rodless drives with steel powder based SLM
Stainless steel with density of 99,5%, part size up to 45 x 25 x 20 mm³ (1,8“ x 1“ x 0,8“)
Complete process chain for a set of 6 pieces : 1 week (compared to serial MIM process > 4 months)
Early reliabilty in product concept: endurance test with 30 million load cycles
25% reduction of development time
SI-T/Müller-Lohmeier 20Case study: New product development
Piston for redesign of rodless pneumatic cylinder
toolless production of a series of 3 units by metal laser melting (SLM) within 3 days
early reliabilty in product concept through immediate testing
avoiding tool costs in case of wrong development direction
Reduction of development time and costs
SI-T/Müller-Lohmeier 21Case study: laser melted aluminium parts
Valve part prototyping for R&D
Valve housing: design study with SLS parts, functional parts with SLM in aluminium
Aluminium parts (AlSi10Mg) with material density of 99,5% / part size up to 145 x 65 x 50 mm³
Complete process chain for 1 piece : 3 days (vs. 8 months by die casting)
But: costs of generative Al part 270 times higher as die casted serial part
High speed support for product development
SI-T/Müller-Lohmeier 22Paradigm shift in design and manufacturing
Manufacturing- Design-driven
driven design manufacturing
• Function integration
• Part number and assembly effort reduction
• New design solutions
Additive manufacturing eventually means the liberation of design from manufacturing
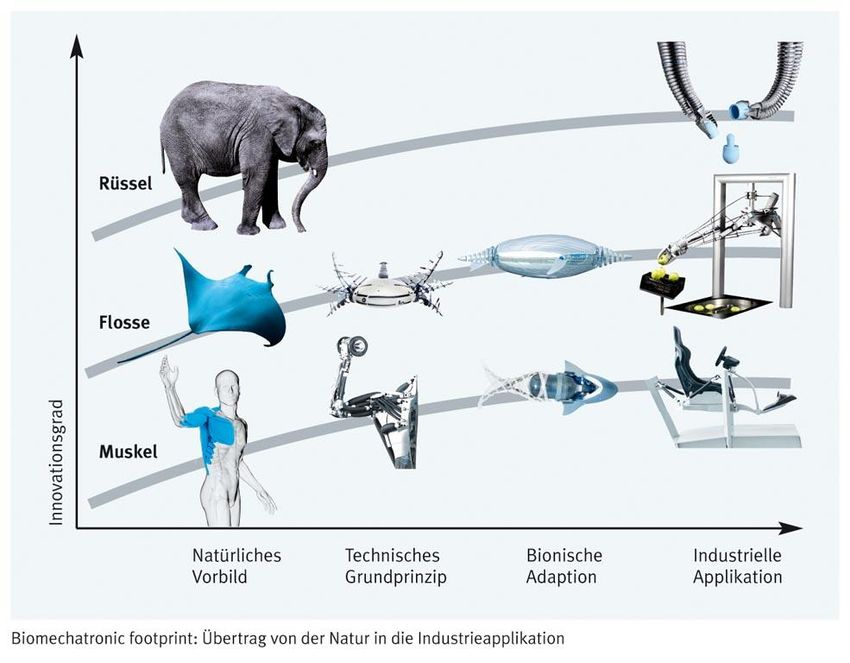
SI-T/Müller-Lohmeier 23Biomechatronic footprint Übertrag von der Natur in die Industrieapplikation SI-T/Müller-Lohmeier
Case study: Support of Bionic Learning Network
FinGripper 2009/ Handling Assistant 2010/ Lightweight Roboter 2010 / Robotino XT 2011
function integration
part number reduction
toolless part fabrication 2010 BHA (2‘)
less or without assembly award
no alternative technology winner RobotinoXT (2‘)
Physical realisation of new handling concepts
SI-T/Müller-Lohmeier 25Adaptive Gripper: A universe of possibilities
Application: Application: Application:
Cookies Chicory Picking and sorting of
pepper
The new gripper picks
autoadaptive and form-locking AG (1‘)
and moves nearly every object
safe and gentle
Fin Ray Effect® is a trademark of EvoLogics, Berlin
SI-T/Müller-Lohmeier 26Case study: laser melted aluminium part
Heat exchanging device for customer specific test bench
Device with internal conformal cooling channels (Al powder-based SLM process)
Part size 244 x 208 x 59 mm³, net weight about 2,5 kg
Non-stop additive manufacturing time : 5 days (complete process chain: 14 days)
Cooling capacity about 8 KW
One of the biggest Al parts in the world done by additive manufacturing
SI-T/Müller-Lohmeier 27Case study: laser melted aluminium part Heat exchanging device for customer specific test bench SI-T/Müller-Lohmeier 28
Typische AM-Baujobs

                       Virtuelle Platzierung von Bauteilen
                       in Baukammern für den
                       Kunststoff-Lasersinterprozess
                       -> optimale Bauraumausnutzung
                       -> werkzeuglose Herstellung
                          geometrisch komplexer Bauteile
                          in größerer Stückzahl

SI-T/Müller-Lohmeier                                         29
„Fazit“
Wir haben das Tor zu der
„Welt von morgen“ durchschritten !
Sind wir wirklich schon mit dem
Rapid bzw. Direct Manufacturing
„im Paradies von morgen“
angekommen ?
SI-T/Müller-Lohmeier
Wintersemester 2010/2011
Sommersemester 2011 30Rapid or Direct Manufacturing
Product operating or service time / customer expectations
Human implants 5-15 years ?
Automation components 6-10 years
Automotive 10-12 years
Aviation 30-40 years
There is a huge difference between Rapid Prototyping and Rapid / Direct Manufacturing !
-> Direct Manufacturing has to face demands from
long-term
„ product liability
„ end-user customer satisfaction and
„ profitability
SI-T/Müller-LohmeierPraxisorientierte Untersuchungen an SLS-Teilen
Wechselbiegung Druckproben/Berstversuche
≥ 5 Millionen Biegewechsel 2,5 mm Wandstärke: 80 bar Berstdruck
SI-T/Müller-Lohmeier 32Grundlagenorientierte Untersuchungen an SLS-Proben und -Material
Zugprüfung und Analyse der Korngrößen- Restmonomergehalt …?
Wechselbiegung an verteilung und Form der und DSC-Analyse
genormten Prüfkörpern Pulverkörner
…?
Basis für begleitende Qualtätssicherung beim Kunststofflasersintern
SI-T/Müller-Lohmeier 33Bauteilversuche mit generativ erzeugten Ventilkörpern aus Aluminium
Pneumatischer Langzeit-Funktionstest Quelle: Festo, BMBF-Förderprojekt AluGenerativ
Prüfkörper: je 2 Ventile mit SLM-Gehäusen in Bauweise H/C bzw. C/H, mechanisch endbearbeitet
Testparameter: ∆p=6 bar, f=3 Hz, Raumtemperatur, Luft nicht geölt
Dauerlaufstart: 06.10.2008 Stand 04.01.2012: 240 Mio. Schaltspiele
Eingangsprüfung: Schaltdrücke: ok Zwischenprüfung: Schaltdrücke: ok
Leckage: ok Leckage: ok
SI-T/Müller-Lohmeier 34Status quo: process (un)reliability !?
Example 1:
Internal crack formation
due to residual stresses ?
Different views of 3D X-ray inspection
Example 2:
Crack formation between support
and part or build plate due to
thermal stresses
SI-T/Müller-Lohmeier 35Abhilfe „SimuSint“
Serien- und Thermomechanische Simulation
generativ erzeugte Quelle: BMBF-Verbundprojekt SimuSint, 2010
Ventilbauteile
Globalmodell Von Mises-Vergleichsspannung Verformungen
-> Simulationssystem zur Berechnung von fertigungsbedingten Temperaturen, Verformungen und
Eigenspannungen von generativ gefertigten Metallteilen
-> Grundlage für Optimierung von Bauparametern (Bauraumorientierung, Stützenausprägung)
-> Reduzierung der Ausfallwahrscheinlichkeit eines Baujobs (Beispiel „5-Tage-Bauteil“ !)
-> Vermeidung von unnötiger Mehrarbeit und Zusatzkosten
-> somit nicht nur gesteigerte Bauteilqualität, sondern auch erhöhte Methodensicherheit durch
Vorab-Simulation des thermomechanischen Wechselspiels
SI-T/Müller-LohmeierKosten-Aspekte bei Kunststoffteilen (PA)
Fangdüse Mitnehmer
1.000,00 € 12,00 €
Kosten RP pro Teil Kosten RP pro Teil
Kosten Spritzguss pro Teil
10,00 €
Kosten Spritzguss pro Teil
100,00 € Kosten Spanend pro Teil
8,00 €
10,00 € 6,00 €
4,00 €
1,00 €
2,00 €
0,10 € 0,00 €
10000
2300
200
400
500
600
700
800
900
1000
1100
1200
1300
1400
1500
1700
1900
2100
2500
2700
2900
3500
4500
1200
1000
1050
1100
1150
1250
1300
1350
1400
1450
1500
1600
1700
1800
1900
2000
2100
2200
2300
2400
2500
2600
2700
2800
2900
3000
3500
4000
4500
5000
10000
Stückzahl
Stückzahl
RM-Benefit bei geometrisch komplexeren Teilen mittlerer Stückzahl (Funktionalität !)
SI-T/Müller-Lohmeier
Wintersemester 2010/2011
Sommersemester 2011 37Kosten- und Zeit-Aspekte bei Metallteilen (Aluminium)
Gehäuse Zeiten:
100.000,00 €
Kosten Rp pro Teil
Sehr lange generative
Kosten Druckguss pro Teil
10.000,00 €
Fertigungszeiten pro Teil:
rund 24 h Bauzeit (Baurate !)
+ 5-7 h kostenintensive Nacharbeit
1.000,00 €
-> 250 Teile -> rund 1 Jahr !
100,00 €
Zum Vergleich
10,00 € -> Werkzeugzeit: 8-10 Monate !
-> ähnliche Kosten bei deutlich
1,00 € höherer Ausbringung
1
8
30
60
90
200
600
750
900
3000
450
1050
1200
1350
1500
1800
2150
2700
2400
4500
Stückzahl
RM-Benefit nur bei kleinsten Stückzahlen („Einzelstückfertigung“) oder „kleinen“ Teilen
SI-T/Müller-Lohmeier
Wintersemester 2010/2011
Sommersemester 2011 38Zusammenfassung
• Es gibt bereits viele beeindruckende Ergebnisse und Erfolge
im RP- und teilweise AM/RM-Bereich !
• Im Gegensatz zum Rapid Prototyping entspricht
der aktuelle Stand des Rapid Manufacturing
aber durchaus noch einer Baustelle !
RM
• Aber: Den Optimisten gehört die Zukunft !
SI-T/Müller-Lohmeier 39Festo Fast Factory … with high expertise and motivation !
Herzlichen Dank für
Ihr Interesse
und
Ihre Aufmerksamkeit
From idea to solution …
… always in top gear !
SI-T/Müller-Lohmeier 40Sie können auch lesen


